
How Large-Scale Directed Energy Deposition Works: Advanced Melt Pool Control and Precision in Deposition
The most advanced Directed Energy Deposition systems today integrate real-time feedback to control material melting, redefining what it means to 3D print with high precision. Thanks to continuous melt pool monitoring, targeted deposition via multi-angle actuators, and dynamic process modeling, large-scale DED overcomes the traditional limits of additive manufacturing, enabling the production and repair of large metal components with unprecedented control over geometry, metallurgical quality, and mechanical properties.
Fundamentals of Directed Energy Deposition
The DED process uses a concentrated energy source to melt metallic material deposited on a substrate, with machine architectures designed to operate on build volumes exceeding one meter in size.
Directed Energy Deposition technology is based on well-defined physical principles: a high-power energy source – a 12 kW laser, electron beam, plasma, or electric arc – is used to create a melt pool on the work surface, into which feedstock material in the form of metal powder or wire is introduced. Unlike powder bed systems, the deposition head is not constrained to a rigid enclosed volume, but can move in three-dimensional space, often mounted on six-degree-of-freedom anthropomorphic robots or large gantry systems.
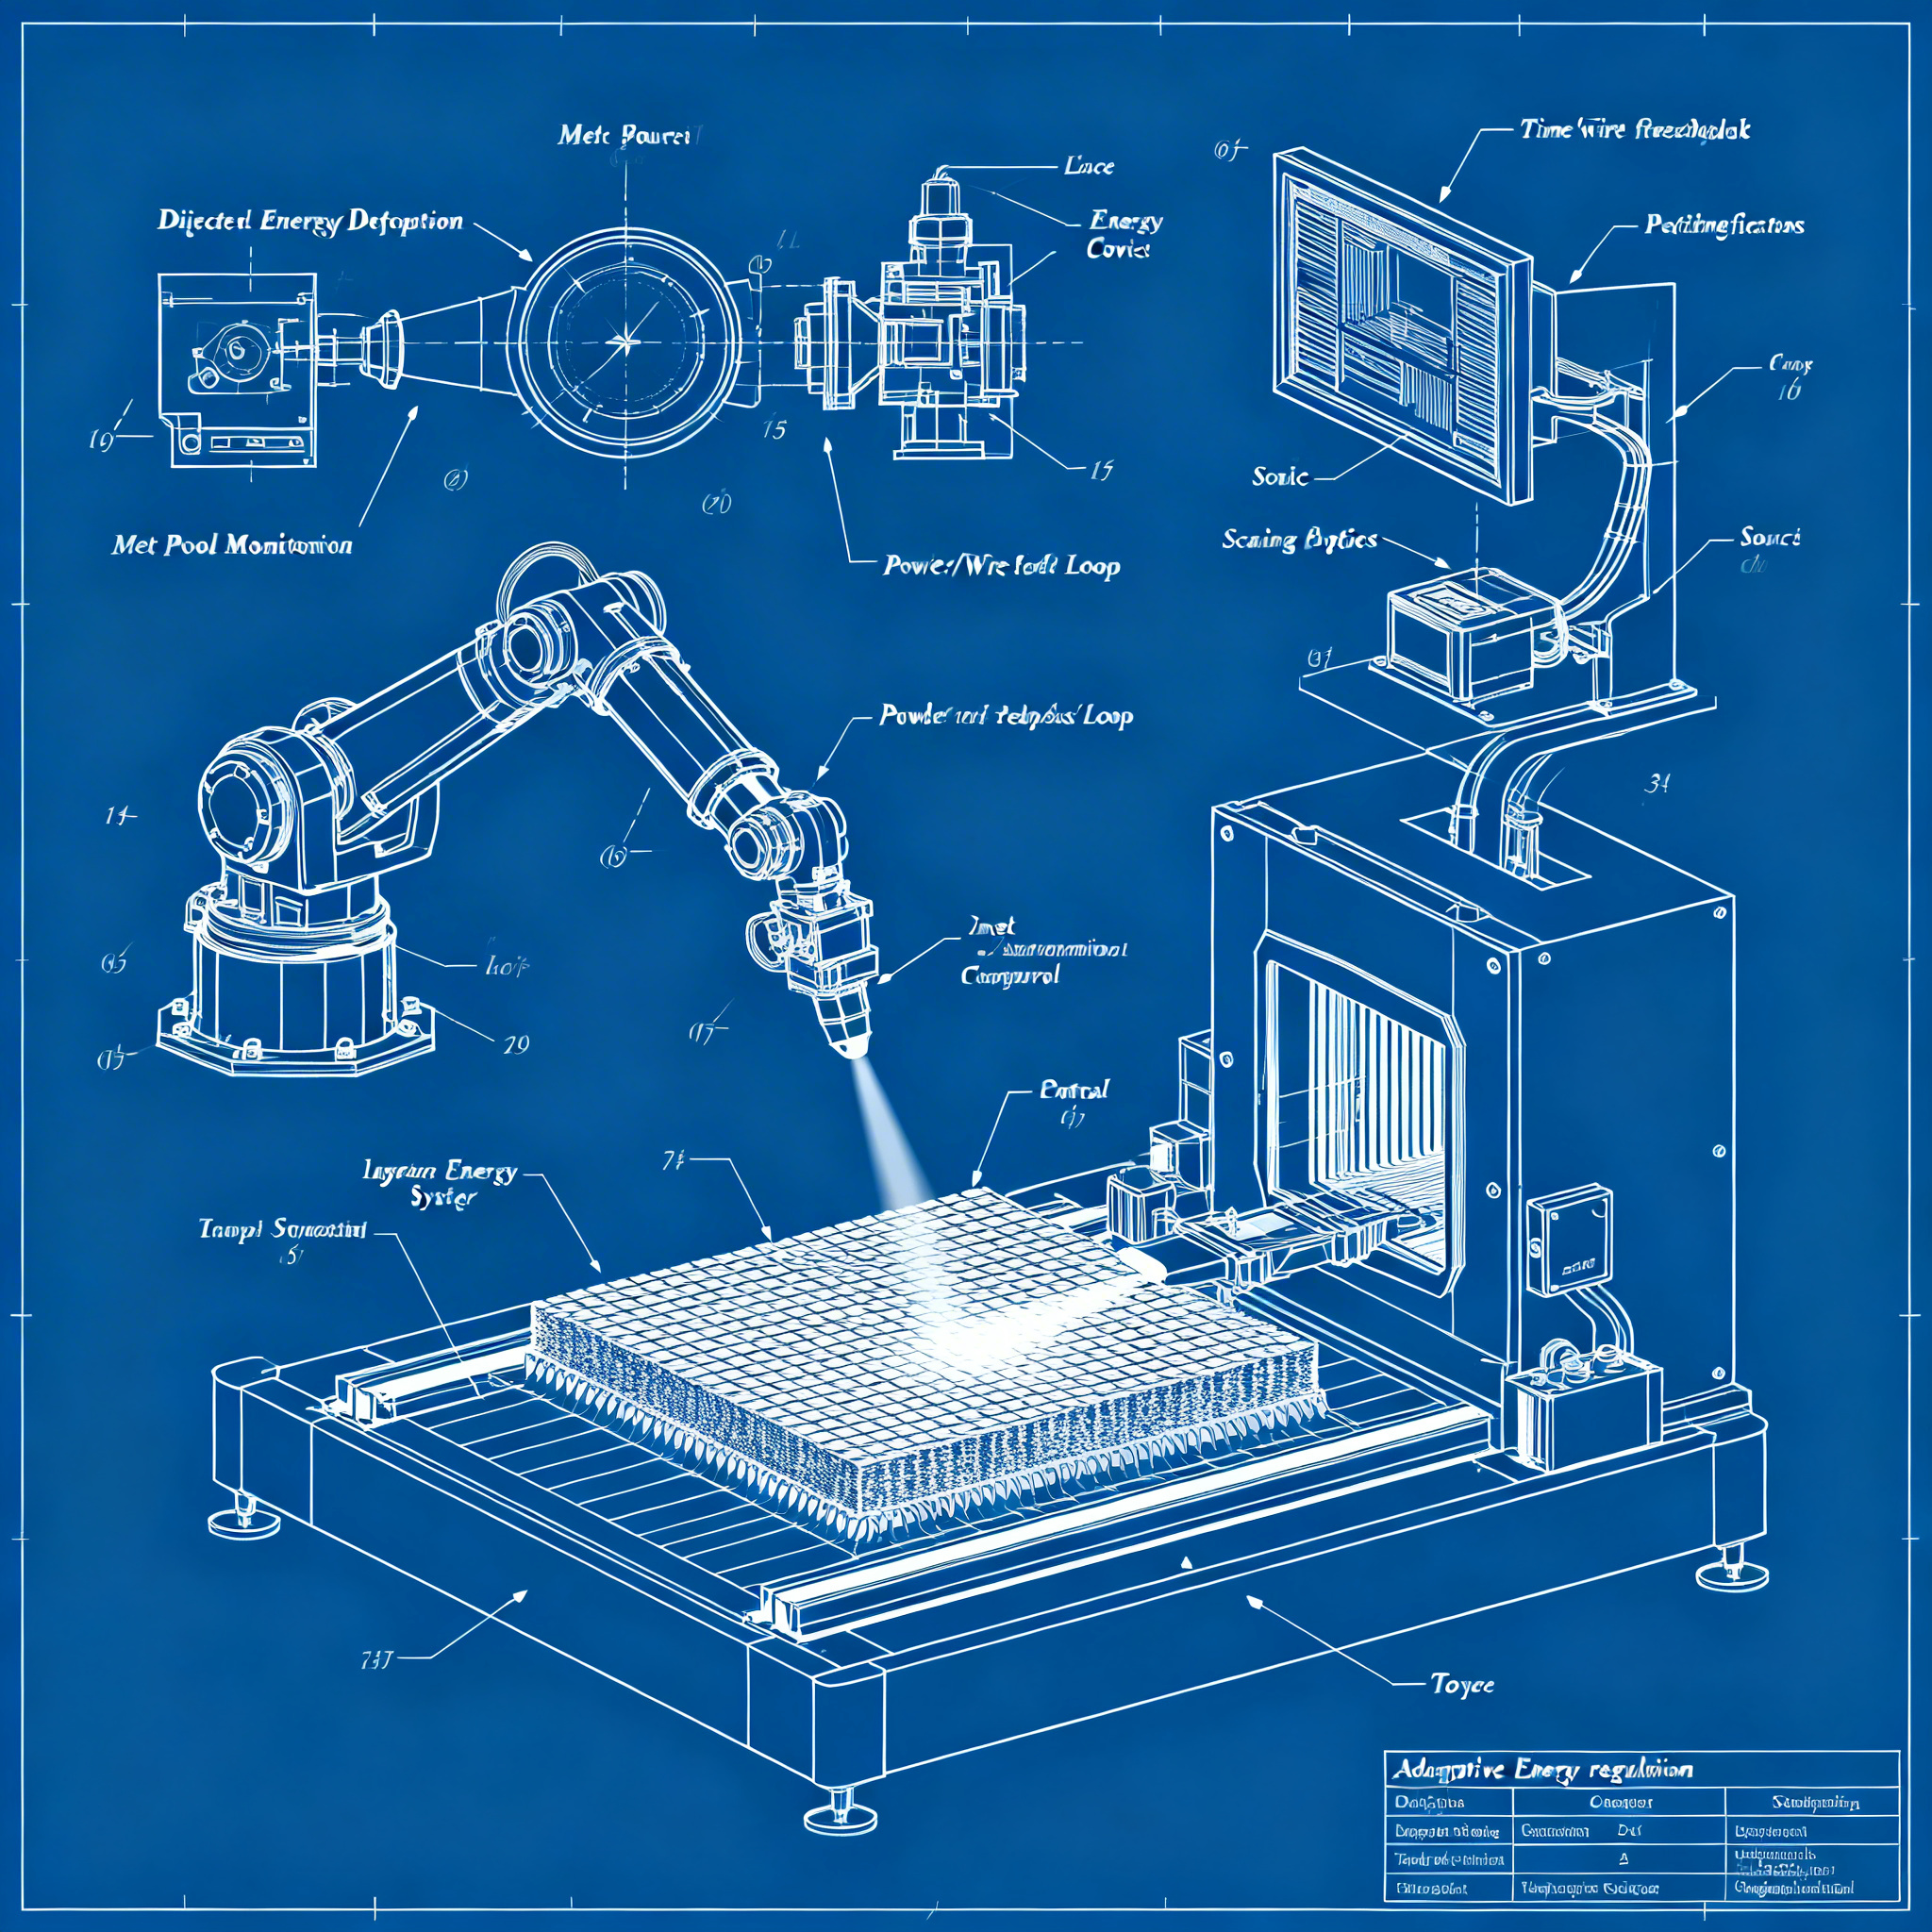
The key components of an advanced DED system include the material deposition nozzle, the energy source with its beam focusing and scanning system, actuators for multi-axis positioning, and real-time monitoring systems. Platforms such as LAMAR (Large Additive Manufacturing Articulating Robot), developed by Penn State and the US Army Research Laboratory, integrate a six-degree-of-freedom robot synchronized with a two-axis rotary positioner, achieving working volumes of 2 m × 3 m × 3.5 m. This kinematic architecture makes it possible to handle complex geometries, manage multi-angle approaches, and optimize deposition trajectories on large components.
For alloys sensitive to oxidation, the most advanced systems operate in controlled chambers with an argon atmosphere, maintaining low oxygen levels to ensure repeatability and certified mechanical properties. Material feeding can occur in single mode, dual-wire for composition-gradient deposits, or hot-wire to improve thermal efficiency by preheating the wire before it interacts with the melt pool.
Real-Time Control of the Melt Pool
Melt pool monitoring technologies and adaptive energy control make it possible to dynamically adjust process parameters to achieve precise molten volume dimensions and ensure consistent deposit quality.
The heart of innovation in advanced DED systems is represented by the melt pool monitor, an observation device that collects real-time data on the characteristics of the melt pool during deposition. These systems detect critical parameters such as melt pool dimensions, surface temperature, shape, and stability of the molten volume, transmitting the information to a computing unit that processes the data and instantly intervenes in the process parameters.
An advanced additive manufacturing system receives from the melt pool monitor data indicative of one or more parameters of the melt pool and determines, based on this data, the current position of the melt pool. The computing unit then establishes the desired melt pool size as a function of the current position and controls the energy delivery device to form a melt pool of the desired size on the component's build surface. This closed feedback loop makes it possible to compensate for thermal variations, geometric irregularities of the substrate, or fluctuations in material flow, keeping deposit quality constant even over long and complex paths.
Adaptive energy regulation occurs by modifying in real time the power of the laser or energy source, the beam scanning speed, or the spatial distribution of energy via two-axis beam scanning systems. This ability to “program” the energy distribution makes it possible to control bead shape, prevent melt pool instability, and optimize penetration and dilution of the deposited material, key elements for achieving controlled metallurgical properties and reducing the need for rework.
Targeted Deposition with Multi-Angle Actuators
Advanced kinematic solutions with actuators positionable at multiple angles enable precise deposition even on complex surfaces, deep cavities, and non-planar geometries, without unwanted remelting of already deposited areas.
A DED system may include a nozzle that deposits metal powder onto a plurality of positions of a repair area, with a first energy source configured to emit a first energy beam from an output end positionable by one or more actuators. These actuators direct the energy beam onto the repair area at a first angle or a second angle relative to the cavity axis, to melt metal powder deposits located in a first set or a second set of the plurality of positions. This ability to vary the angle of the energy beam is crucial for complex repairs, where access to the area to be treated may be limited by surrounding geometries or deep cavity walls.
The in-situ automatic toolpath generation technology developed by FormAlloy represents a significant evolution: through real-time scanning and coordinate registration, the system establishes accurate spatial alignment of the part geometry with respect to the machine coordinate system, without manual intervention. Once alignment is established, deposition paths are generated in situ to conform to the measured surface geometry, enabling deposition closely coupled to the actual condition of the part rather than to an idealized model.
This automated approach reduces excess material, minimizes post-processing operations, and improves dimensional control, proving particularly effective when components exhibit dimensional variability introduced during machining, casting, forging, or in-service wear. The closed-loop nature of this workflow supports consistent results even when parts show batch-to-batch or part-to-part variability, making DED viable on an industrial scale.
Dynamic Process Modeling
Real-time simulation systems integrated into advanced DED platforms continuously optimize process parameters based on data collected during deposition, predicting thermal behavior, residual stresses, and final microstructure.
The convergent approach to large-scale DED integrates numerical process modeling with closed-loop control, creating an ecosystem in which materials, hardware, software, and control converge toward the ability to deposit material repeatably. Thermal and mechanical models predict deposition, dilution, and residual stresses, while optimization algorithms suggest suitable parameters in advance to combine high deposition rates with acceptable microstructures.
These computational systems dynamically model the process based on parameters observed by the melt pool monitor and other integrated sensors, adapting preheating strategies, thermal control, and deposition sequences to reduce temperature gradients on very large components. Predictive modeling makes it possible to define toolpath strategies suited to large-format complex surfaces, limiting overbuilding and rework, and to develop materials dedicated to DED thermal dynamics with attention to segregation, grain size, and microstructural stability over multiple passes.
The integration of non-destructive testing (NDT) in-process or post-process, to identify porosity, cracks or lack of fusion, completes the picture of an intelligent system capable of ensuring that mechanical properties and metallurgical quality are aligned with design requirements. This convergence between simulation, adaptive control and real-time verification represents the qualitative leap that makes large-scale DED an industrially mature technology, capable of competing with traditional manufacturing and repair methods both on costs and on time.
Conclusion
Large-scale DED represents a frontier of additive manufacturing where precision and advanced control merge to overcome traditional limits. The integration of continuous melt pool monitoring, multi-angle actuators for targeted deposition and dynamic process modeling transforms metal 3D printing from an experimental technology into a concrete industrial solution for large components. The ability to adapt process parameters in real time to the actual condition of the part, combined with the possibility of operating on build volumes greater than one meter with certifiable metallurgical control, opens application scenarios ranging from turbine repair to the production of primary aerospace structures.
Discover how these technologies are transforming sectors such as aerospace and heavy industry, where the combination of the ability to build in large format and the possibility of integrating subtractive finishing operations leads to a new supply chain logic: instead of keeping stocks of massive components, smaller batches can be produced or restored, with greater flexibility and customization.
article written with the help of artificial intelligence systems
Q&A
What are the main components of an advanced Directed Energy Deposition system?
The key components include the material deposition nozzle, the energy source with beam focusing and scanning system, multi-axis positioning actuators, and real-time monitoring systems. These elements work together to ensure precision and control during the deposition process.
How does real-time melt pool control work in advanced DED systems?
The melt pool monitor collects real-time data on the characteristics of the molten pool, such as size, temperature, and stability. This information is processed by a computing unit that dynamically adjusts process parameters, such as beam power and speed, to maintain consistent deposit quality.
What advantages do multi-angle actuator solutions offer in deposition?
Multi-angle actuators allow material to be deposited on complex surfaces, deep cavities, and non-planar geometries without remelting previously deposited areas. This flexibility is particularly useful for complex repairs with limited access to the treatment areas.
What is the role of dynamic process modeling in large-scale DED systems?
Dynamic modeling integrates real-time simulations with sensory data to predict thermal behavior, residual stresses, and final microstructure. This approach enables continuous optimization of process parameters, improving the quality of the final component and reducing necessary rework.
How does large-scale DED overcome the limitations of traditional additive manufacturing?
Large-scale DED allows for the production and repair of large metallic components with advanced control over geometry, metallurgical quality, and mechanical properties. It uses real-time feedback, targeted deposition, and dynamic modeling to achieve superior precision and repeatability compared to traditional methods.


