
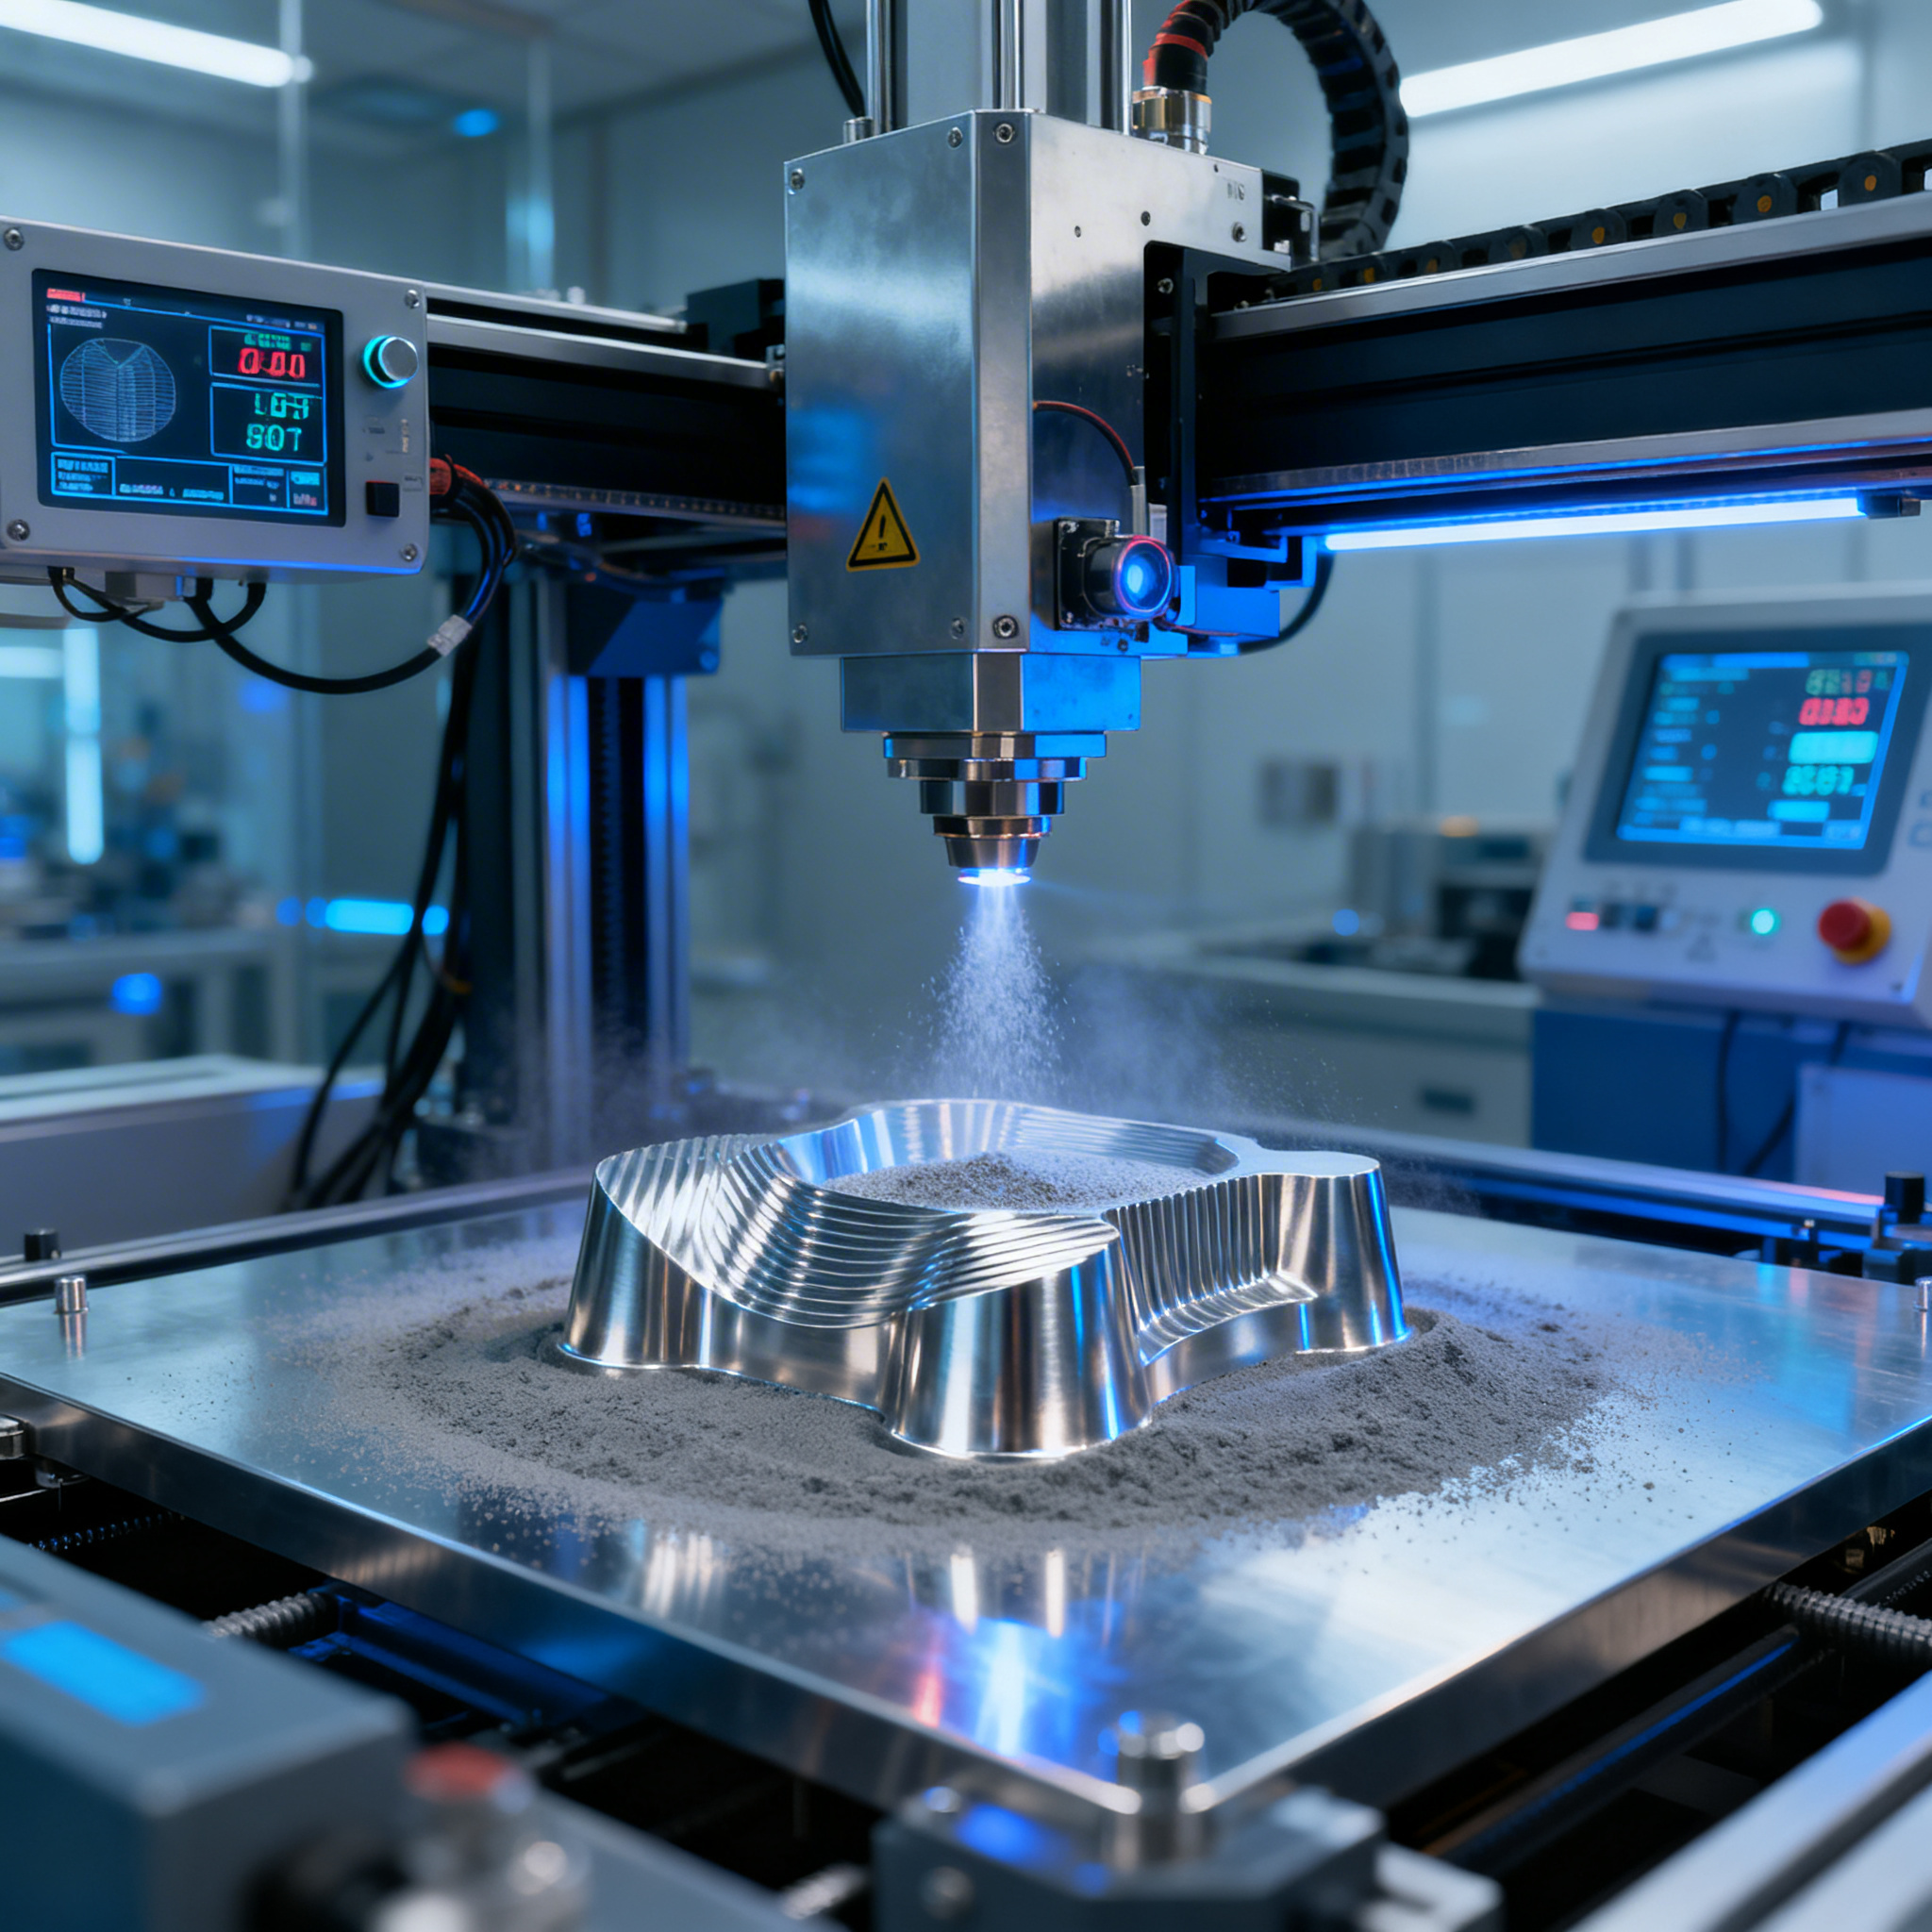
Powder under control: how patents are redefining precision in additive manufacturing
At the heart of new technologies for additive manufacturing is a silent revolution: intelligent powder control, which promises to make every layer more precise and predictable.
Patents cited
- POWDER MONITORING FOR ADDITIVE MANUFACTURING SYSTEMS — 2025-09-04
- POWDER MONITORING FOR ADDITIVE MANUFACTURING SYSTEMS — 2025-09-04
What problem does it solve
The variability of powder properties can compromise the quality of the final product, causing defects that are difficult to predict or correct after the fact.
In metal 3D printing, every layer depends on the quality and consistency of the deposited powder. When particle characteristics vary—size, morphology, flowability—the result can be an unstable melt pool, unwanted porosity, or structural defects that emerge only after costly post-printing processing. The first patent describes a system that receives data from sensors and determines particle characteristics, generating signals that make it possible to adapt deposition parameters in real time. The second patent focuses on the flow characteristics of the powder: the system receives data from sensors, determines the flow properties, and generates signals to control both the energy delivery device and the powder feeding device.
The challenge is not only technical: it is economic. Every part scrapped due to powder-related defects represents wasted machine hours, material, and post-processing. In sectors such as aerospace, where components must pass rigorous qualifications, feedstock variability can halt entire production runs.
The idea in 60 seconds
Two recent patents propose active powder monitoring systems during 3D printing, with the goal of dynamically adapting process parameters based on the actual conditions of the material.
Both patents describe additive manufacturing systems that include an energy delivery device (to form the melt pool on the build surface), a powder feeding device (which directs a powder flow toward the melt pool), at least one sensor, and a computing unit. The difference lies in the focus: the first system analyzes particle characteristics—size, shape, distribution—and adapts the laser energy or deposition speed to maintain optimal melting conditions. The second system monitors the powder flow characteristics—flow rate, uniformity, direction—and adjusts the parameters to ensure that every layer receives the right amount of material, in the right place, at the right time.
In both cases, the computing unit receives data from the sensors, processes it, and controls the energy and powder devices to deposit a plurality of layers according to a set of deposition parameters. The approach is closed-loop: the system “sees” what is happening and reacts, instead of relying on predefined parameters that do not account for actual variations in the material.
What really changes (tangible improvements)
Thanks to real-time monitoring, waste is reduced, consistency between layers improves, and post-printing corrections are minimized.
The first system, focused on particle characteristics, makes it possible to detect when the powder has irregularities—for example, particles that are too large or agglomerates—and to compensate by modifying the energy delivered or the deposition parameters. This results in improved layer quality and reduced waste due to powder irregularities. If the powder changes during printing (for example, due to contamination, moisture, or degradation from reuse), the system adapts the process instead of producing a defective part.
The second system, focused on flow, addresses a different but equally critical problem: variability in the amount of powder that reaches the melt pool. Even with powder of excellent quality, if the flow is irregular—too much or too little material—the result is a non-uniform layer. Continuous flow monitoring allows for greater uniformity between layers and reduces the need for corrective post-processing, such as mechanical rework or heat treatments to correct dimensional or structural defects.
Both systems aim for more repeatable production: less variability means fewer surprises, fewer trials, less waste. For those producing in series, this translates into more predictable costs per part and a wider process window, facilitating the adoption of new alloys or recycled powders.
Esempio in azienda / sul mercato
In advanced contexts such as aerospace, prototypes that regulate laser energy or distributor speed based on collected data are already in use.
Let’s imagine an aeronautical manufacturing department that prints nickel alloy components. During printing, the particle monitoring system detects that a portion of the powder has a slightly different particle size distribution from the previous batch—perhaps due to a supplier change or degradation from reuse. The system automatically adapts the laser energy to maintain optimal fusion, avoiding porosity or bonding defects between layers.
In another scenario, an automotive manufacturer prints a complex component with variable geometries. The flow monitoring system detects a variation in the powder flow rate—perhaps due to a partial clog or a fluctuation in the carrier gas pressure. The system immediately corrects the speed of the powder distributor, ensuring that each area of the layer receives the correct amount of material.
These examples are not yet market standards, but they represent the type of application that patents make possible. The technology is based on sensors that can already be integrated into existing systems and on feedback loops already used in other automated industrial sectors, which makes adoption plausible in the coming years.
Trade-offs and limitations
Implementation requires structural modifications to existing machines and raises questions about sensor reliability in thermally aggressive environments.
The first limitation is integration: both systems require sensors, computing units, and control software that are not standard on all AM machines. For manufacturers with legacy machine fleets, adoption could mean expensive retrofits or replacement of equipment. The complexity of integration with existing machinery is a real obstacle, especially for companies that have already invested in process qualifications based on fixed parameters.
The second limitation concerns the long-term reliability of sensors in a high-temperature environment: the melt pool can exceed 1,500 °C, and the surrounding environment is often saturated with fine powder, inert gases, and radiation. Optical or thermal sensors must withstand these conditions without degrading or requiring continuous calibration. The need for continuous calibration for different types of powder is another critical point: every alloy, every supply, every batch can have different characteristics, and the system must be “trained” or configured to recognize and handle these variations.
Finally, there is the risk of possible interference with other optical measurements in the working field: many AM machines already use melt pool or layer surface monitoring systems. Adding additional sensors for the powder could create conflicts or redundancies, requiring a more complex system architecture.
Reality check: what is needed to reach production
Real adoption will require prolonged test cycles, common standards for integration, and specific training for operators.
Patents describe working systems, but the transition from paper to production requires validation. Prolonged test cycles are needed on different alloys, different machines, different operating conditions. AM machine manufacturers will have to collaborate with sensor and software suppliers to define standardized system architectures, avoiding proprietary solutions that fragment the market.
Another critical element is training: operators will need to understand how to interpret the system’s signals, how to intervene in case of anomalies, how to configure parameters for new alloys or new powder batches. Intelligent powder control does not eliminate human expertise, but shifts it to a different level: from “recipe executor” to “supervisor of adaptive systems”.
Finally, a data ecosystem is needed: to train predictive models and validate correlations between powder characteristics and part quality, shared databases, industry benchmarks, and collaborations among manufacturers, powder suppliers, and research centers are needed. Without this layer of shared knowledge, every company will have to reinvent the wheel, slowing adoption.
Toward more reliable processes and less prone to human error
Intelligent powder control represents a concrete step forward toward more reliable processes and less subject to human error. It is not a miracle solution: it requires investments, skills, and adequate infrastructure. But for companies operating in high-precision sectors—aerospace, medical, energy—the ability to adapt the process in real time, instead of discovering defects after printing is complete, can make the difference between a qualified component and a rejected one.
Companies that invest in these technologies now will be able to count on greater competitiveness in high-precision sectors, reducing waste, improving repeatability, and accelerating the adoption of new alloys and recycled powders. Intelligent powder monitoring is not just an addition of sensors: it is a change in approach to process control, moving additive manufacturing from a craft art to a measurable and predictable science.
article written with the help of artificial intelligence systems
Q&A
What are the main issues that variations in powder properties can cause during metal 3D printing?
Variations in powder properties, such as size, morphology, and flowability, can lead to an unstable melt pool, unwanted porosity, and structural defects. These problems can compromise the quality of the final product and require costly post-printing machining.
What do the two patents mentioned in the article consist of?
The first patent describes a system that monitors the characteristics of powder particles and adjusts deposition parameters in real time. The second patent focuses on monitoring powder flow, regulating energy delivery and powder feeding devices to ensure uniformity and precision in layers.
How do these systems contribute to improving additive manufacturing?
Both systems reduce waste, improve layer consistency, and minimize post-print corrections. By monitoring powder characteristics and flow in real time, the systems can compensate for irregularities, increasing process repeatability and lowering per-part costs.
What are the main limitations and challenges related to implementing these systems?
Key limitations include the need for structural modifications to existing machinery, sensor reliability in thermally aggressive environments, and the complexity of integration with already installed systems. Additionally, frequent calibration and specific operator training may be required.
Which sectors could benefit most from this technology?
Sectors such as aerospace and automotive, where component quality and precision are critical, can greatly benefit from this technology. Specifically, monitoring systems help avoid structural defects and produce components compliant with strict specifications without relying on repeated post-production inspections.


